
Machine-translated by Google. Questions are authored in English.
Top

Arc Welding Processes Questions and Answers

1.

Which welding process employs a continuously fed electrode and uses both an external gas source and a granular flux to protect the weld pool?

Exam Year(s)

DSSSB - 2023,

Answer: C

Flux-cored arc welding employs a continuously fed electrode and uses both an external gas source and a granular flux for protecting the weld pool in the key. The electrode is a tube filled with flux. Gas metal arc welding uses a continuously fed wire and an external gas, but no flux, plasma arc welding uses a tungsten electrode and a plasma gas, and electro gas welding is used for vertical joints with a separate gas shield.

The difference from gas metal arc welding is the flux core in the wire, which forms slag over the weld metal.

Please log in or register to report this question.
2.

In an arc welding process, welding speed is doubled. Assuming all other process parameters to be constant, the cross sectional area of the weld bead will

Exam Year(s)

GATE ME - 2017,

Answer: D

The bead cross-section will reduce by 50%.

With all other parameters fixed, the volume of filler deposited per unit time is constant. The bead area times the welding speed equals that deposition rate, so the cross-sectional area is inversely proportional to the travel speed:

\[ A_{2} = A_{1}\frac{v_{1}}{v_{2}} = \frac{A_{1}}{2} \]

The heat input per unit length (VI/v) also halves for the same reason. A 25% reduction would correspond to a speed increase of one third, and the bead cannot grow when the same metal is spread over a longer length.

Please log in or register to report this question.

3.

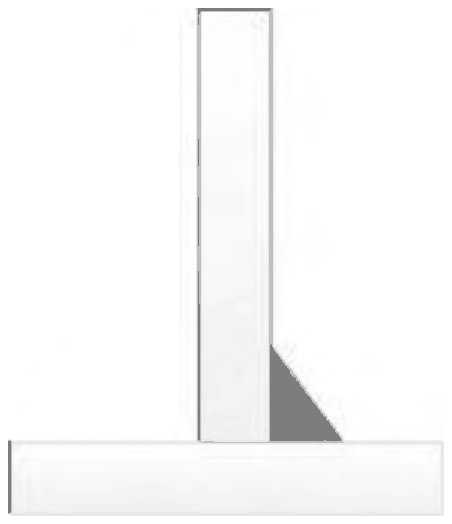
The type of weld represented by the shaded region in the figure is

T-joint: a vertical plate standing on a horizontal plate, with a shaded triangle filling the corner between them on one side

Exam Year(s)

GATE ME - 2018,

Answer: C

The shaded weld is a fillet weld.

The figure shows a T-joint, one plate standing on another at right angles, with a triangular weld bead filling the corner between them. A weld of roughly triangular cross-section laid in the corner of a T, lap or corner joint is a fillet weld, the most common type.

A groove weld is laid in a prepared gap between the edges of the parts. Spot welds are small resistance-welded nuggets between overlapping sheets. A plug weld fills a hole in one plate to join it to the plate beneath. None of these forms a triangle in a corner.

Please log in or register to report this question.

4.

In a DC arc welding operation, the voltage-arc length characteristic was obtained as \(V_{arc}=20+5l\) where the arc length l was varied between 5 mm and 7 mm. Here Varc denotes the arc voltage in Volts. The arc current was varied from 400 A to 500 A. Assuming linear power source characteristic, the open circuit voltage and the short circuit current for the welding operation are

Exam Year(s)

GATE ME - 2012,

Answer: C

The open circuit voltage is 95 V and the short circuit current 950 A.

A longer arc needs more voltage and so draws less current from a drooping source. The two operating points are:

\[ \begin{aligned} l = 5:\ V &= 45\ \text{V},\ I = 500\ \text{A} \\ l = 7:\ V &= 55\ \text{V},\ I = 400\ \text{A} \end{aligned} \]

A linear source characteristic through both points has slope \(-10/100 = -0.1\) V/A:

\[ \begin{aligned} V &= V_{oc} - 0.1I \\ 45 &= V_{oc} - 50 \Rightarrow V_{oc} = 95\ \text{V} \\ I_{sc} &= 95/0.1 = 950\ \text{A} \end{aligned} \]

Pairing the short arc with the low current instead gives a rising line that has no meaningful open circuit voltage, and 45 V is just the arc voltage at 5 mm. 75 V and 150 V do not pass through both operating points.

Please log in or register to report this question.

5.

The most suitable electrode material used for joining low alloy steels using Gas Metal Arc Welding (GMAW) process is

Exam Year(s)

GATE ME - 2024,

Answer: C

The most suitable electrode material is low alloy steel.

GMAW (MIG/MAG welding) uses a continuously fed consumable wire electrode, which melts and becomes the filler metal in the joint. For low alloy steels the wire is chosen to match the base metal's composition and strength, so a low alloy steel wire is used.

Tungsten is the non-consumable electrode of gas tungsten arc (TIG) welding, not GMAW. Copper is used for contact tips and resistance-welding electrodes, and cadmium has no use as a welding electrode; neither would give a sound steel weld.

Please log in or register to report this question.

Loading…
Tags: Arc Welding Processes Questions and Answers || Arc Welding Processes MCQ Questions and Answers || Arc Welding Processes GK Questions and Answers || Arc Welding Processes GK MCQ Questions || Arc Welding Processes Multiple Choice Questions and Answers || Arc Welding Processes GK || GK on Arc Welding Processes || Metal Casting and Welding Questions and Answers || Metal Casting and Welding MCQ Questions and Answers || Metal Casting and Welding GK Questions and Answers || GK on Metal Casting and Welding