
Machine-translated by Google. Questions are authored in English.
Top

Machining and Cutting Tools Questions and Answers

1.

Which machine tool employs an endless, looped blade to perform the cutting action, particularly suited for irregular or curved shapes?

Exam Year(s)

DSSSB - 2023,

Answer: A

A bandsaw employs an endless looped blade to cut, and it is suited to irregular and curved shapes. A shaper and a planer use a single point tool in a reciprocating motion for flat surfaces, and a slotter is a vertical shaper for cutting slots and keyways, so none of them uses an endless blade. The key therefore gives the bandsaw.

Please log in or register to report this question.
2.

Using the Taylor’s tool life equation with exponent \(n = 0.5\), if the cutting speed is reduced by 50%, the ratio of new tool life to original tool life is

Exam Year(s)

GATE ME - 2018,

Answer: A

The new tool life is 4 times the original.

Taylor's equation is \(VT^{n} = C\). With n = 0.5:

\[ \begin{aligned} \frac{T_{2}}{T_{1}} &= \left(\frac{V_{1}}{V_{2}}\right)^{1/n} \\ &= 2^{1/0.5} = 2^{2} = 4 \end{aligned} \]

Halving the speed doubles \(V_{1}/V_{2}\), and the exponent 1/n = 2 squares that ratio. 2 is what a linear relation (n = 1) would give, and 0.5 or 1 would mean slower cutting shortened or did not change tool life.

Please log in or register to report this question.
3.

Details pertaining to an orthogonal metal cutting process are given below.

Chip thickness ratio0.4
Undeformed thickness0.6 mm
Rake angle+10°
Cutting speed2.5 m/s
Mean thickness of primary shear zone25 microns

The shear strain rate in s-1 during the process is

Exam Year(s)

GATE ME - 2012,

Answer: C

The shear strain rate is about \(1.0104\times10^{5}\) s-1.

First the shear angle, from the chip thickness ratio r = 0.4 and rake angle 10°:

\[ \begin{aligned} \tan\phi &= \frac{r\cos\alpha}{1-r\sin\alpha} = \frac{0.3939}{0.9305} \\ &= 0.4233,\ \phi = 22.94^{\circ} \end{aligned} \]

The shear velocity along the shear plane is:

\[ \begin{aligned} V_{s} &= \frac{V\cos\alpha}{\cos(\phi-\alpha)} = \frac{2.5(0.9848)}{\cos 12.94^{\circ}} \\ &= 2.526\ \text{m/s} \end{aligned} \]

Dividing by the shear zone thickness of 25 microns gives the strain rate:

\[ \begin{aligned} \dot{\gamma} &= \frac{2.526}{25\times10^{-6}} \\ &= 1.0104\times10^{5}\ \text{s}^{-1} \end{aligned} \]

Dividing the cutting speed itself by the zone thickness gives exactly \(1.0\times10^{5}\), near but not equal to the keyed value; the velocity that slides across the shear zone is the shear velocity, not the cutting speed. The other three options do not follow from these data.

Please log in or register to report this question.

4.

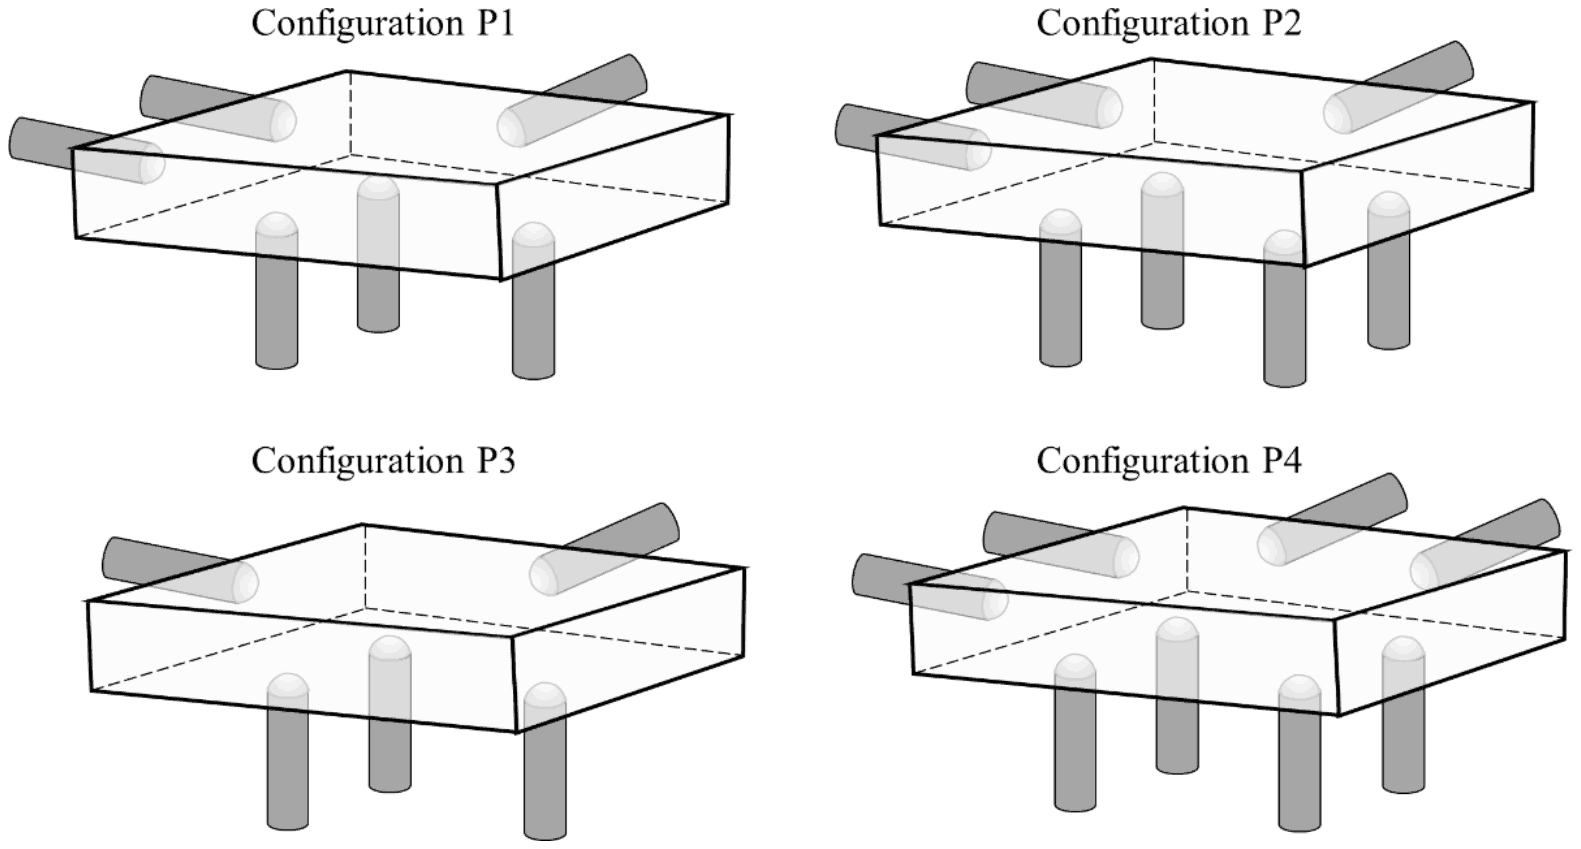
A cuboidal part has to be accurately positioned first, arresting six degrees of freedom and then clamped in a fixture, to be used for machining. Locating pins in the form of cylinders with hemi-spherical tips are to be placed on the fixture for positioning. Four different configurations of locating pins are proposed as shown. Which one of the options given is correct?

Four drawings of a cuboid resting on locating pins, labelled Configuration P1, P2, P3 and P4

Exam Year(s)

GATE ME - 2023,

Answer: A

The correct statement is that Configuration P1 arrests 6 degrees of freedom, while P2 and P4 are over-constrained and P3 is under-constrained.

A cuboid is located by the 3-2-1 principle: three pins under the largest face fix one translation and two rotations, two pins on a side face fix a further translation and rotation, and one pin on the adjacent end face fixes the last translation, six points for six degrees of freedom.

  • P1: three pins below and three on the sides, in the 3-2-1 pattern, so exactly 6.
  • P2: four pins below and three on the sides, 7 in all; one is redundant, so it is over-constrained.
  • P3: three below and only two on the sides, 5 in all; one freedom is left, so it is under-constrained.
  • P4: four below and four on the sides, 8 in all; over-constrained.

Each of the other options puts the correct 3-2-1 label on a configuration with too many or too few pins.

Please log in or register to report this question.

5.

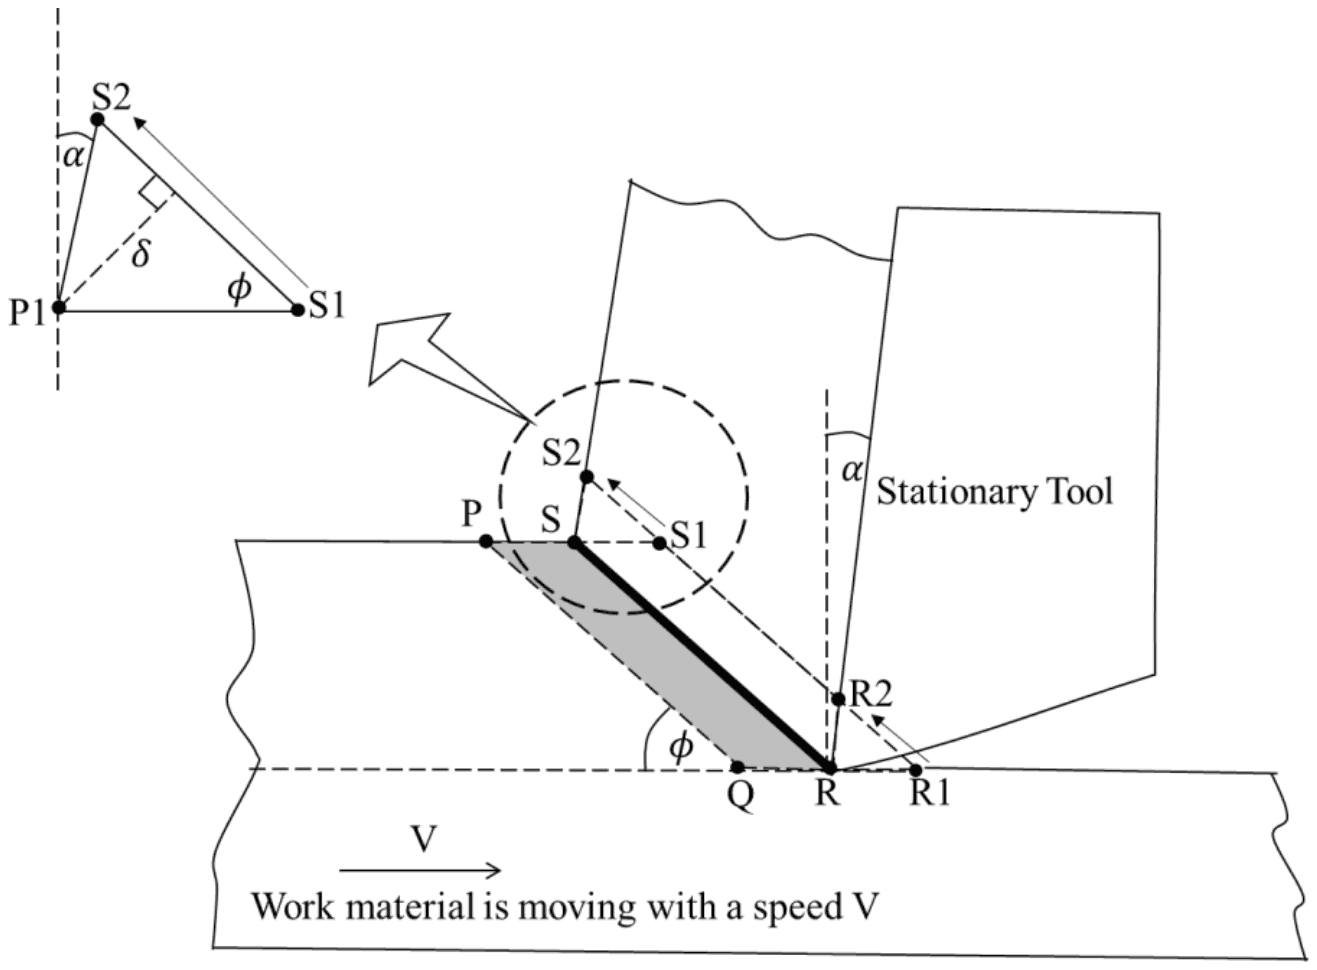
In an ideal orthogonal cutting experiment (see figure), the cutting speed V is 1 m/s, the rake angle of the tool \(\alpha\) = 5°, and the shear angle, \(\phi\), is known to be 45°.

Applying the ideal orthogonal cutting model, consider two shear planes PQ and RS close to each other. As they approach the thin shear zone (shown as a thick line in the figure), plane RS gets sheared with respect to PQ (point R1 shears to R2, and S1 shears to S2).

Assuming that the perpendicular distance between PQ and RS is \(\delta\) = 25 μm, what is the value of shear strain rate (in s-1) that the material undergoes at the shear zone?

Orthogonal cutting: work moving right at speed V into a stationary tool of rake angle alpha, shear planes PQ and RS at shear angle phi, with an enlarged sketch of S1 shearing to S2 across distance delta

Exam Year(s)

GATE ME - 2023,

Answer: B

The shear strain rate is \(5.20 \times 10^{4}\ \text{s}^{-1}\).

The strain rate is the shear velocity along the shear plane divided by the thickness of the shear zone. From the velocity triangle of orthogonal cutting,

\[ \begin{aligned} V_{s} &= \frac{V\cos\alpha}{\cos(\phi - \alpha)} \\ &= \frac{\cos 5^{\circ}}{\cos 40^{\circ}} \\ &= \frac{0.9962}{0.7660} \\ & = 1.300\ \text{m/s} \end{aligned} \]

\[ \begin{aligned} \dot{\gamma} &= \frac{V_{s}}{\delta} \\ &= \frac{1.300}{25 \times 10^{-6}} \\ &= 5.20 \times 10^{4}\ \text{s}^{-1} \end{aligned} \]

The distractors reuse numbers from the same calculation. 1.84 is the shear strain, \(\cot\phi + \tan(\phi - \alpha) = 1 + 0.839\), a dimensionless quantity, not a rate. 1.30 is the shear velocity in m/s; dividing it by 100 μm instead of 25 μm would give \(1.30 \times 10^{4}\). 0.71 is \(\cos 45^{\circ}\), which does not give the strain rate on its own.

Please log in or register to report this question.

Loading…
Tags: Machining and Cutting Tools Questions and Answers || Machining and Cutting Tools MCQ Questions and Answers || Machining and Cutting Tools GK Questions and Answers || Machining and Cutting Tools GK MCQ Questions || Machining and Cutting Tools Multiple Choice Questions and Answers || Machining and Cutting Tools GK || GK on Machining and Cutting Tools || Manufacturing Technology Questions and Answers || Manufacturing Technology MCQ Questions and Answers || Manufacturing Technology GK Questions and Answers || GK on Manufacturing Technology